What Is a Metal Detector for the Pharmaceutical Industry?
A metal detector for pharmaceutical industry applications is an in-line inspection system designed to identify metallic contamination in tablets, capsules, powders, and packaged medicines. It typically generates an electromagnetic field and detects disturbances caused by ferrous, non-ferrous, or stainless-steel particles. The equipment may sit after a tablet press, before bottling, or beside a conveyor carrying sealed packs. That distinction matters.
Pharmaceutical manufacturers treat contamination control as a quality-system responsibility, not merely an equipment purchase. The U.S. FDA’s current Good Manufacturing Practice requirements, including 21 CFR Parts 210 and 211, emphasize suitable facilities, process controls, testing, and documented quality decisions. EU GMP Annex 1 also places strong emphasis on contamination-control strategies, risk assessment, and ongoing monitoring. In addition, the International Society for Pharmaceutical Engineering’s guidance on commissioning and qualification supports documented installation, testing, and performance verification. These sources establish the framework; they do not guarantee perfect detection.
Industry data reinforces the need for disciplined inspection. PMMI’s pharmaceutical and medical-device packaging reports describe continued investment in automation, serialization, and inspection technologies. Recent ISPE and PDA technical guidance similarly highlights lifecycle management, data integrity, and risk-based validation. A detector must therefore be tested with certified reference samples, challenged at defined intervals, and connected to an effective reject mechanism. No detector is infallible. Product effect, moisture, speed, aperture size, and stainless-steel characteristics can reduce sensitivity. Operators still need training, review, and documented corrective action. This article explains how the technology works, where it fits within pharmaceutical manufacturing, and why validation should remain practical, evidence-based, and honest about its limitations.
Pharmaceutical Metal Detectors: Purpose, Scope, and GMP Role
What Is a Metal Detector for the Pharmaceutical Industry?
Pharmaceutical Metal Detectors: Purpose, Scope, and GMP Role
A pharmaceutical metal detector identifies metallic contamination in tablets, capsules, powders, and other processed products. It commonly detects ferrous, non-ferrous, and stainless-steel particles. These particles may enter during milling, compression, blending, or equipment maintenance. A small fragment can damage product quality and patient confidence.
Its purpose extends beyond simple detection. Under GMP practice, the system supports contamination control, documented procedures, and batch traceability. Operators should challenge the detector with approved test pieces during setup, product changeover, and scheduled checks. The reject device must respond correctly. Records should show the result, operator, time, and any corrective action.
The scope has limits. Product moisture, conductivity, temperature, and packaging can reduce sensitivity. A detector cannot replace equipment inspection, supplier controls, or effective cleaning. It also cannot identify every foreign material. That assumption can fail. In practical production, teams sometimes test only at the beginning of a run. This creates a weak control point. A stronger approach uses product-specific validation, routine verification, alarm review, and documented investigation of every rejected unit. GMP expectations also require controlled procedures, trained personnel, calibration, and careful handling of deviations. The best performance depends on disciplined use, not equipment alone.
How Electromagnetic Detection Identifies Fe, Non-Fe, and Stainless Steel
What Is a Metal Detector for the Pharmaceutical Industry?
Electromagnetic detection separates metal contaminants by their magnetic and electrical behavior. Ferrous metals, such as iron, create strong magnetic signals and are usually easiest to detect. Non-ferrous metals, including aluminum and copper, produce conductive signals without strong magnetic attraction. Stainless steel is more difficult. Its weak conductivity can create a smaller signal, especially in wet or salty products.
In pharmaceutical production, detectors inspect tablets, capsules, powders, and liquid-filled packs. A transmitter creates an electromagnetic field across the inspection aperture. When metal interrupts that field, the receiver measures the signal change and activates a reject mechanism. The 2024 Fortune Business Insights metal detector market report estimated the global market at approximately USD 1.1 billion in 2023. That figure reflects wider industrial demand, not pharmaceutical performance alone.
Detection sensitivity depends on aperture size, line speed, product effect, and detector frequency. USP General Chapter <1058> supports documented instrument qualification, while FDA current good manufacturing practice principles require controlled and suitable equipment. Operators should challenge systems with certified ferrous, non-ferrous, and stainless-steel test pieces. Stainless steel often needs more careful validation. A single factory test is not enough. Real products vary between batches, and our assumptions can fail. Calibration records, reject confirmation, and routine trend reviews reveal those weaknesses.
Typical 0.5–2.0 mm Test Spheres for Pharmaceutical Sensitivity Checks
What Is a Metal Detector for the Pharmaceutical Industry?
Typical 0.5–2.0 mm Test Spheres for Pharmaceutical Sensitivity Checks
A pharmaceutical metal detector checks tablets, capsules, powders, and other products for unwanted metallic particles. It creates an electromagnetic field inside the inspection aperture. When metal passes through, the signal changes and may trigger rejection. The detector is only one part of contamination control. Product handling, equipment maintenance, and documented checks also matter.
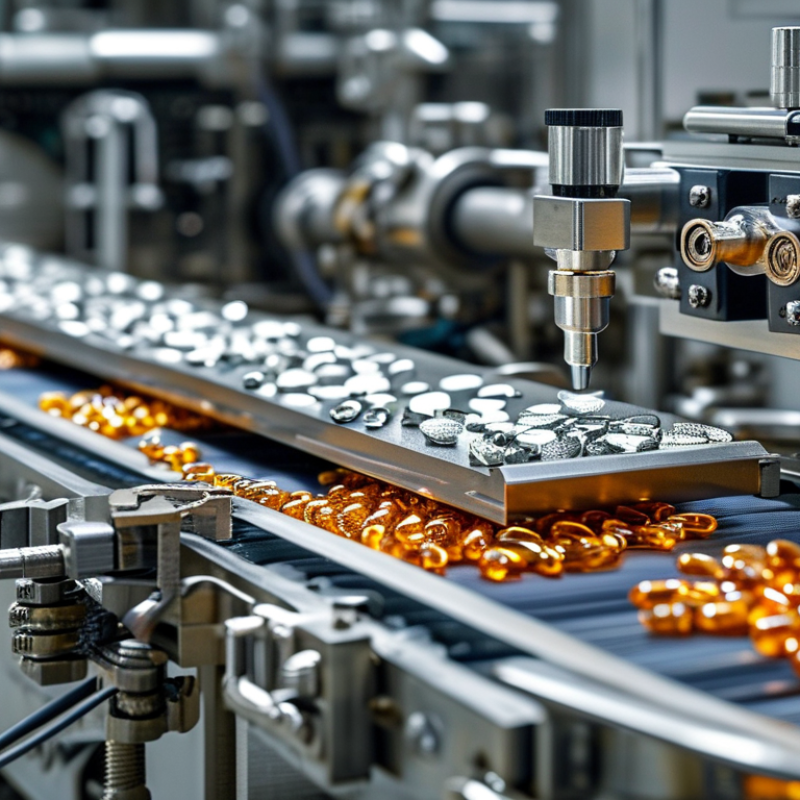
Sensitivity checks often use certified test spheres measuring 0.5, 0.8, 1.0, 1.5, or 2.0 mm. Smaller spheres create a tougher challenge. However, the smallest sphere is not automatically the best choice. Product density, moisture, temperature, speed, and aperture size can affect detection performance. Ferrous, non-ferrous, and stainless-steel spheres should be selected according to the product risk and validation plan.
A technician usually places the test sphere in the product stream, rather than passing it alone. This method reflects real operating conditions. The test should cover the center and relevant edges of the aperture, because sensitivity may vary across the opening. Checks are commonly performed during start-up, at defined intervals, after product changes, and after maintenance. Failed tests require product isolation and an investigation, not a quick reset.
Small details matter. A loose test sphere can be difficult to control. Labels can fade. Records can become incomplete. These weaknesses are easy to overlook during a busy shift. A reliable program uses traceable spheres, clear procedures, trained operators, and reviewable test records. Yet even a strong procedure deserves periodic questioning, because real production conditions rarely stay perfectly consistent.
What Is a Metal Detector for the Pharmaceutical Industry? - Typical 0.5–2.0 mm Test Spheres for Pharmaceutical Sensitivity Checks
Reference data for routine sensitivity verification of pharmaceutical product inspection systems
| Test Sphere Diameter |
Typical Test Material |
Primary Detection Purpose |
Common Pharmaceutical Application |
Expected Challenge Level |
Recommended Verification Point |
| 0.5 mm |
Ferrous steel |
High-sensitivity ferrous detection |
Small tablets, capsules, powders, and granules |
Very high |
Routine start-up or post-cleaning check where the validated limit is 0.5 mm |
| 0.7 mm |
Ferrous steel |
Verification of stable ferrous sensitivity |
Compressed tablets and coated tablets |
High |
Beginning and end of a production run |
| 1.0 mm |
Ferrous steel |
Standard ferrous sensitivity confirmation |
Tablets, capsules, sachets, and dry ingredients |
High |
Routine challenge test at defined production intervals |
| 1.0 mm |
Non-ferrous metal, commonly brass |
Verification of non-ferrous detection |
Dry powders and products with moderate electrical conductivity |
Moderate to high |
Use with the product that represents the most difficult operating condition |
| 1.5 mm |
Non-ferrous metal, commonly brass |
Routine non-ferrous sensitivity check |
Capsules, tablets, and packaged pharmaceutical products |
Moderate |
Periodic verification when the validated limit is 1.5 mm |
| 1.5 mm |
Stainless steel, typically austenitic grade |
Detection of difficult-to-detect stainless-steel contamination |
Products with high moisture, salt, or conductivity |
Very high |
Challenge under the most conductive product conditions |
| 2.0 mm |
Ferrous steel |
Basic ferrous detection confirmation |
Bulk powders, large tablets, and filled containers |
High |
Routine operational check where a 2.0 mm limit is validated |
| 2.0 mm |
Stainless steel, typically austenitic grade |
Confirmation of stainless-steel detection capability |
Moist or conductive pharmaceutical formulations |
Very high |
End-of-run check or verification after product changeover |
Important testing note:
The actual detectable size depends on detector aperture, product effect, product temperature, line speed, orientation, packaging, and validated operating conditions. Test spheres should be certified, traceable, securely encapsulated, and passed through the detector in the product stream according to the site’s approved procedure. A test sphere diameter is not a universal performance guarantee.
Validation Under 21 CFR Parts 210–211 and EU GMP Requirements
What Is a Metal Detector for the Pharmaceutical Industry?
A pharmaceutical metal detector identifies metallic fragments in tablets, capsules, powders, or finished packs. It supports foreign-matter control, not product quality by itself. Typical systems challenge ferrous, non-ferrous, and stainless-steel test pieces during validation. Operators record detection, rejection, alarm, and restart performance.
Validation must align with 21 CFR Parts 210–211. Section 211.68 requires appropriate checks for automated equipment, while Sections 211.100 and 211.160 support written procedures and scientifically sound controls. The FDA Process Validation Guidance (2011) describes three lifecycle stages: process design, qualification, and continued process verification. Therefore, testing should cover installation, operating limits, product effects, and routine monitoring.
EU GMP Annex 15 requires documented qualification and validation. EU GMP Chapter 5 also expects effective controls against contamination and cross-contamination. A practical protocol may include challenge tests at start-up, after product changeover, and after maintenance. It should verify detection sensitivity, reject confirmation, alarm visibility, and failed-test handling. Records need traceability, reviewer signatures, and deviation assessments.
Small details matter.
A damp powder can reduce sensitivity. Packaging may create a false signal. Temperature changes can also affect performance. These risks require documented studies, not assumptions. The FDA’s Data Integrity guidance (2018) reinforces complete, consistent, and attributable records. A common weakness remains overreliance on a single successful test. Continued verification should examine trends, rejects, alarms, and unexplained downtime. No detector can compensate for poor sampling or weak operator training.